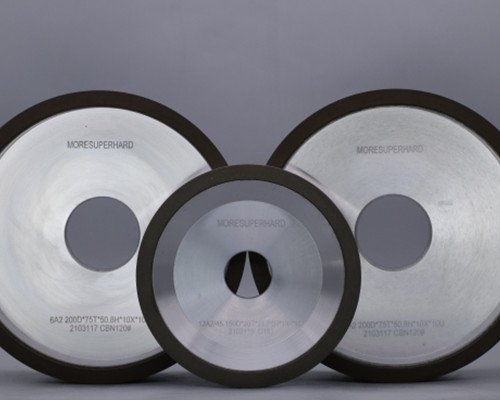
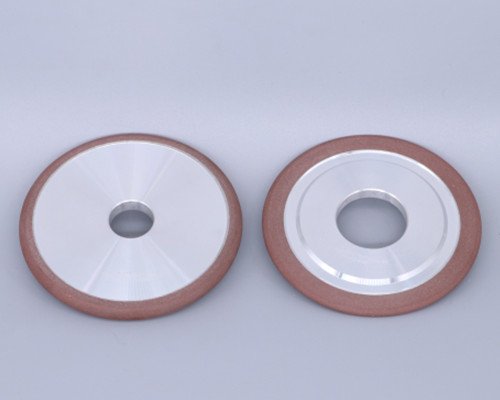
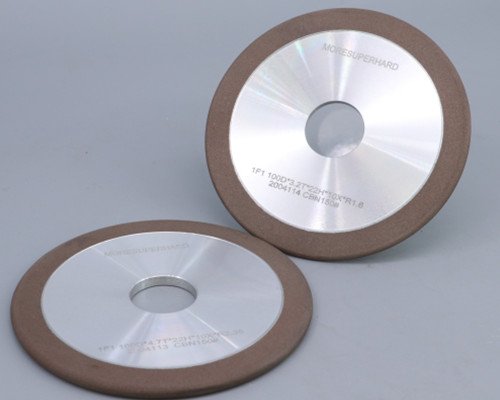


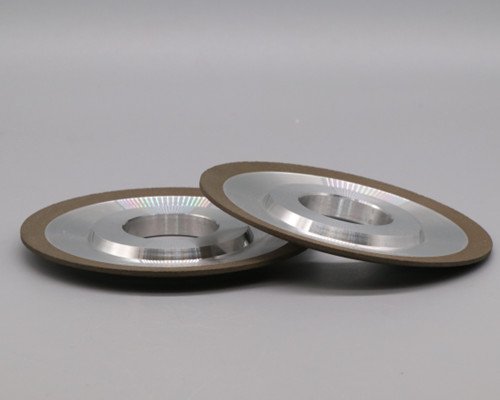

Our resin CBN grinding wheels cover full grinding processes for high-speed steel broach tools, including profile radius forming, front face, flute gashing and clearance relief grinding.
The 1F1 radius profile wheel is our flagship for circular broach resharping on manual grinders. We also supply 1A1, 14E1, 14F1 resin CBN wheels for CNC broach grinders, supporting keyway broaches, spline broaches, surface broaches and round broaches.
Perfect upgrade to replace conventional alumina wheels, reducing wheel change frequency, thermal burn and workshop downtime.
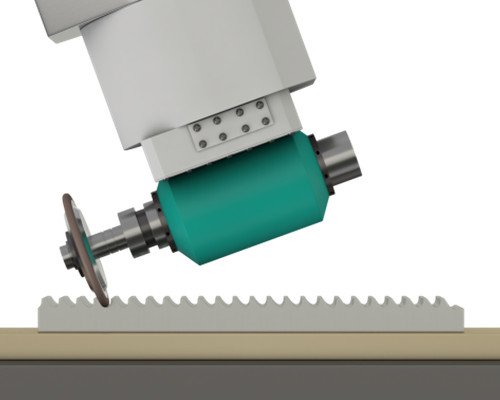
| Wheel Shape | Main Grinding Application | Machine Type |
|---|---|---|
| 1F1 | Radius profile forming, circular broach resharpening (core product) | Manual broach grinder |
| 1A1 | Flat face grinding, front face rough/finish grinding, peripheral relief | CNC broach grinder / Tool grinder |
| 14E1 | Flute gashing, clearance angle grinding, complex profile broach | CNC broach grinder (Vollmer etc.) |
| 14F1 | Special form profile, spline & keyway broach forming | CNC profile grinding machine |

| Series | Models | Abrasive Grain | Remark |
|---|---|---|---|
| 1F1‑D40 Mainstream Broach Series | 1F1 D40 T6 W8 H8 R3 | CBN | Standard broach resharpening |
| 1F1 D40 T4 W8 H8 R2 | |||
| 1F1 D40 T3.2 W8 H8 R1.6 | |||
| 1F1 D40 T2.6 W8 H8 R1.3 | |||
| 1F1 D40 T2 W6 H8 R1 | |||
| Dry Grinding Optimized D75 Series (Full‑Arc T=2R) |
1F1 D75 W10 H9.5 R2.0 | CBN B120 C125 | Full arc profile, dry grinding optimized |
| 1F1 D75 W10 H9.5 R2.5 | |||
| 1F1 D75 W10 H9.5 R3.0 | |||
| 1F1 D75 W10 H9.5 R3.5 | |||
| 1F1 D75 W10 H9.5 R4.5 | |||
| Regular Multi‑Size 1F1 Models | 1F1 D75 T6 W8 H20 R3 | CBN | General broach regrinding |
| 1F1 D75 T4 W8 H20 R2 | |||
| 1F1 D100 T6 W8 H20 R3 | |||
| 1F1 D50 T5 W8 H13 R2.5 | |||
| 1F1 D30 T2.6 W8 H8 R1.3 | |||
| 1F1 D30 T2 W8 H8 R1 |
| Wheel Shape | Available Size Range | Abrasive | Bond | Application |
|---|---|---|---|---|
| 1A1 | D75 / D100 / D125 / D150 | CBN | Polyimide / Phenolic | Broach front face, peripheral relief grinding |
| 14E1 | D100 / D125 / D150 / D200 | CBN | Polyimide / Phenolic | Flute gashing, clearance angle grinding |
| 14F1 | D100 / D125 / D150 | CBN | Polyimide / Phenolic | Spline broach, keyway broach profile forming |
Custom sizes available: D25, D50, D75, D100, D125, D150, D200, small batch acceptable
Bond choice: Polyimide Resin / Phenolic Resin; Grain customizable: B100, B120, B150, B180, B240 etc.
| Workpiece | High‑speed steel broach tools: circular broach, keyway broach, spline broach, surface broach |
| Process | Broach new tooth forming, flute gashing, front face grinding, clearance relief, resharpening / regrinding |
| Suitable Machine | Manual broach sharpening machine, CNC broach grinder (Vollmer, etc.) |
| Grinding Condition | Dry grinding (no coolant) / Wet grinding (oil / emulsion coolant) |
A: Polyimide resin bond: Preferred for dry grinding, high temperature resistance, low thermal burn risk, ideal for manual broach sharpening.
Phenolic resin bond: Cost-effective, good wet grinding performance, high profile stability, suitable for CNC broach grinders with oil coolant.
A: Yes, our polyimide resin CBN wheels are specially formulated for dry grinding of HSS broaches. Phenolic bond wheels are recommended for wet grinding for longer lifespan.
A:
If you are unsure, send us your broach drawing and grinding machine model, we will recommend the matching wheel.
A: Yes, test samples are available. We support small trial order before bulk purchase. Sample lead time is about 5–7 working days for standard profiles.
A: Standard 1F1 profiles: 3–5 working days. Custom profile wheels (1A1 /14E1 /14F1): within 10 working days.
A: B120 is the most popular general-purpose grade for HSS broach resharpening. B100 for heavy stock removal; B150/B180/B240 for fine finishing.
A: Yes, same mounting hole size can be used directly. You only need to adjust grinding parameters: lower feed rate and less frequent dressing.
Customer Background: Independent broach reconditioning shop, mainly resharpens HSS circular broaches on manual grinders, dry grinding without coolant. Previously used conventional alumina wheels.
Pain Points: Alumina wheel wears extremely fast, only 2 broaches per wheel; frequent wheel replacement, high consumable cost and frequent downtime.
Our Solution: 1F1 D40 & D75 polyimide resin bond CBN wheels, CBN B120 C125, full arc T=2R profile.
Result: Single wheel can resharpen 22–28 pcs broaches, over 10× longer service life than alumina; profile stays consistent, no frequent re-dressing; no thermal burn on HSS broach cutting edge; annual stable order: 300–400 pcs.
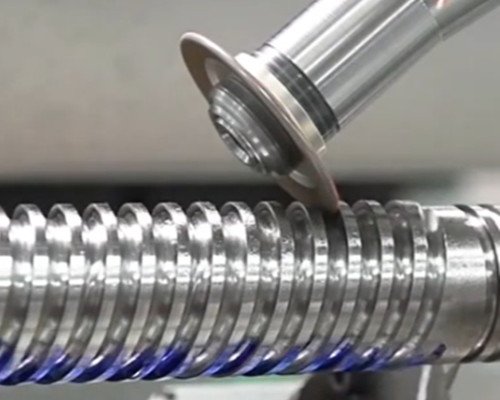
Share your broach drawing, grinding process, machine type and target quantity. Our technical team will recommend the correct wheel shape and reply with quotation within 24 working hours.