Home > Industry Solutions > Electroplated CBN Grinding Wheels: Practical Gear‑Grinding Case Study on Liebherr LGG‑280

13

Oct

Electroplated CBN Grinding Wheels: Practical Gear‑Grinding Case Study on Liebherr LGG‑280

18
Share:

Gear grinding demands micron‑level precision, consistent grinding performance and well‑controlled finished tooth profile. For high‑speed grinding of heat‑treated high‑hardness gears, electroplated CBN (EP‑CBN) grinding wheels serve as an effective superabrasive solution compatible with high‑end Liebherr LGG series gear grinding machines. It resolves conflicts between accuracy and productivity in mass production of hardened alloy steel gears.

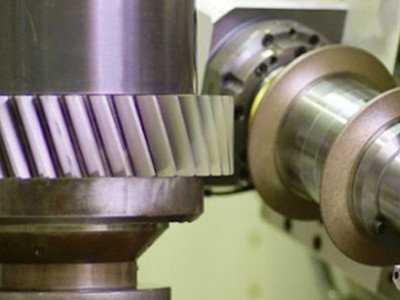
This case focuses on heat‑treated 16MnCr5 HH gears (58‑63 HRC) tested on the Liebherr LGG‑280 gear grinder with up‑grinding method. A combined shaft‑mounted electroplated CBN wheel set for roughing and finishing is applied. Fully repeatable process parameters are provided as practical reference for gear manufacturing in automotive transmission and construction machinery sectors.
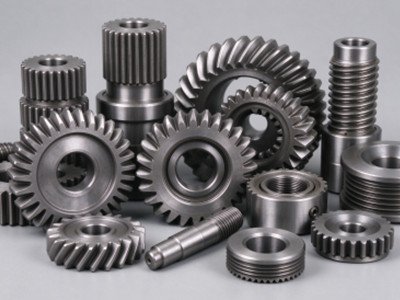
gear for different industry gear grinding

Project Conditions & Machine Setup

  • Workpiece Material: 16MnCr5 HH carburized‑quenched gear
  • Workpiece Hardness: 58‑63 HRC
  • Grinding Machine: Liebherr LGG‑280 Gear Grinding Machine
  • Grinding Method: Up‑Grinding
  • Wheel Configuration: Combined shaft‑mounted electroplated CBN wheels. One roughing wheel and one finishing wheel are assembled on one shaft. One shaft end is fixed at the operator side and the other at the machine side, enabling both roughing and finishing operations in a single clamping setup.

Benefits of combined shaft‑mounted design: Reduces wheel change‑over and truing time, eliminates positioning errors from repeated re‑clamping, and suits high‑volume continuous gear grinding production.

Validated Grinding Process Parameters

Grinding Parameter Roughing Finishing
Cutting Speed 33 m/s 33 m/s
Feed Rate 1800 m/min 1800 m/min
Spindle Speed 7,638.4 rpm 7,638.4 rpm
Grinding Method Up Grinding Up Grinding
Number of Strokes 1 2
Stock Removal per Stroke – Flank 0.060 mm 0.015 mm
Total Stock Removal 0.120 mm 0.060 mm

Process Notes: Roughing removes heat‑treatment induced stock rapidly. Finishing adopts two grinding strokes with light depth of cut to guarantee tooth profile accuracy and surface finish. The consistent cutting speed of 33 m/s for both roughing and finishing simplifies machine parameter switching and improves overall process stability.

Why Choose Electroplated CBN for Gear Grinding?

Electroplated CBN wheels integrate the superior thermal resistance and wear resistance of CBN grains with precisely‑controlled single‑layer electroplated bonding layer. It delivers prominent performance for precision gear grinding scenarios where strict wheel geometry and grain protrusion are critical.

  1. High‑speed grinding capability for hardened ferrous materialsCBN features good chemical inertness to ferrous alloys. Under 33 m/s high‑speed grinding conditions, it effectively prevents grinding burn and works perfectly for 58‑63 HRC quenched gears.
  2. Superior profile replication accuracyElectroplating technology reproduces target grinding profiles directly onto wheels. No on‑machine dressing is required. Excellent profile retention ensures consistent tooth geometry across mass‑produced gears.
  3. High grain exposure for efficient material removalThe single‑layer electroplated structure maintains high abrasive grain protrusion. Sharp cutting edges make full contact with workpieces for efficient cutting and chip evacuation while avoiding wheel loading.
  4. Flexible customised applicationWheel profile and hub construction can be customised to match various gear geometries, machine interfaces and process requirements. For premium gear grinders such as Liebherr LGG‑280, Moresuperhard supplies custom shaft‑mounted combined wheel assemblies integrating roughing and finishing functions.

Important Reminder: Electroplated CBN wheels are single‑layer abrasive tools and cannot be dressed. Final gear quality heavily depends on substrate machining and electroplating manufacturing precision in the pre‑production phase.

electroplated cbn grinding wheel for gear gear grinding wheel

Moresuperhard Project Implementation Approach

Instead of supplying off‑the‑shelf standard wheels, Moresuperhard technical team delivers complete custom wheel solutions according to customer workpiece material, gear drawing tolerances, LGG‑280 mounting dimensions and stock allocation:
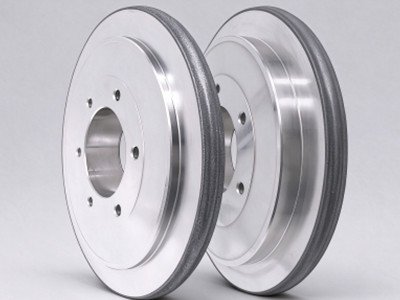
  1. Evaluate spindle and shaft mounting dimensions to design integrated rough‑finish wheel shaft assembly;
  2. Select proper CBN grain size and electroplating parameters separately for high‑stock roughing and high‑precision finishing;
  3. Deliver complete parameter sheets including spindle speed, cutting speed, stroke strategy and stock removal distribution;
  4. Conduct on‑site process validation, optimise stroke cycles and mitigate risks such as tooth burn and profile out‑of‑tolerance.

electroplated cbn grinding wheel for crv gear

Frequently Asked Industry Questions

Q1: What applications fit electroplated CBN gear grinding wheels?
A: It is ideal for high‑speed precision grinding of heat‑treated hardened alloy steel gears, especially for high‑volume production where on‑machine wheel dressing is unavailable, minimal tool‑change downtime and high batch consistency are expected. It is not recommended for heavy‑impact heavy‑stock grinding that requires repeated dressing cycles.
Q2: Is 33 m/s mandatory for grinding 16MnCr5 HH gears?
A: 33 m/s is the validated cutting speed from this field case. Minor adjustments are allowed on basis of cooling condition, abrasive grit size and gear module. Too low cutting speed may trigger grinding chatter, while excessive speed accelerates electroplated layer wear.
Q3: What are pros and cons of shaft‑mounted combined wheels compared with separate single wheels?
A: Advantages: Complete roughing and finishing within one clamping cycle; less truing‑related error and shorter auxiliary time. Drawbacks: Higher assembly cost; full shaft assembly needs disassembly and inspection if either roughing or finishing wheel wears out.
Q4: Which key factors influence electroplated CBN wheel service life?
A: Cutting speed, stock removal per stroke, cooling performance and workpiece hardness. Excessive depth of cut per pass causes electroplated coating peeling. Sufficient grinding coolant greatly extends wheel working life.

Summary & Service Inquiry

Field tests on Liebherr LGG‑280 with 16MnCr5 HH quenched gears prove that custom shaft‑mounted combined electroplated CBN wheels from Moresuperhard reliably complete full rough‑to‑finish grinding cycles with practical, ready‑to‑use process parameters. This solution addresses critical challenges for high‑precision mass production of hardened gears.

Whether you aim to replace existing imported wheels, optimise current grinding processes or develop new gear production lines, Moresuperhard provides custom‑built electroplated CBN grinding wheels and process parameter support according to your machine model, workpiece material and gear geometric tolerances.

Contact our technical team for your custom EP‑CBN grinding wheel solution for gear‑grinding projects.
Source: Moresuperhard Alan Electroplated CBN Wheel Field Case. All working conditions and process parameters are derived from real‑world machine trials.
También podría ser de su interés
electroplated cbn grinding wheel

Electroplated CBN Grinding Wheel for Inconel

Our Electroplated CBN Grinding Wheels are specifically designed for high-efficiency machining of nickel-based superalloys such as Inconel 718, GH4169, and Waspaloy.
tech@moresuperhard.com
008617700605088