05
Aug
Reworking a resin bond diamond grinding wheel can help restore its working profile and grinding performance. However, improper dressing, excessive material removal, wheel damage, or unsuitable grinding conditions may lead to scratches, chatter marks, and inconsistent surface roughness.
This guide explains the common causes of poor surface finish after resin bond diamond wheel rework, how to identify the source of the problem, and what to check before returning the wheel to production.
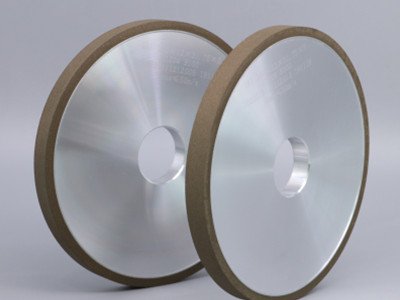
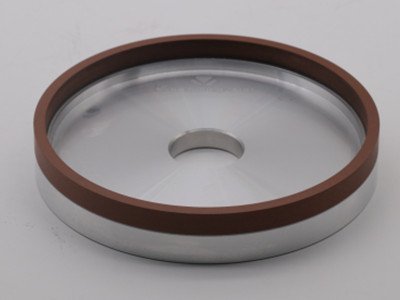
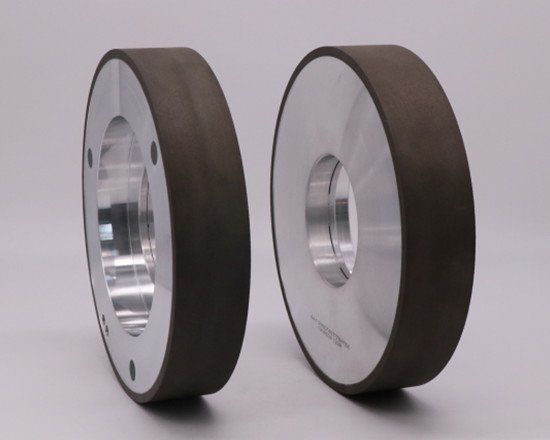
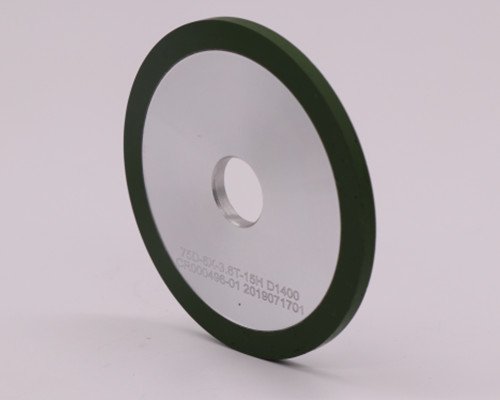
Resin bond diamond grinding wheels are used for precision machining of cemented carbide, advanced ceramics, glass, and other hard materials. Depending on the wheel design and application, suitable dressing or reconditioning procedures may help restore the working surface or profile.
Rework should not be confused with routine dressing. Dressing generally conditions the working surface to improve abrasive exposure and cutting behavior. Reconditioning may involve additional inspection or repair, depending on the wheel construction and the damage present.
Not every resin bond diamond wheel can be safely or economically reworked. The remaining abrasive layer, bond condition, wheel geometry, mounting design, and manufacturer’s recommendations should be evaluated before any corrective operation.
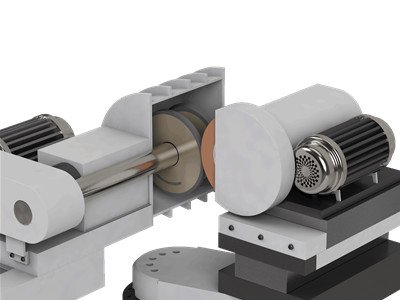
Poor surface finish does not always mean that the grinding wheel itself is defective. The following symptoms can help identify possible causes.
These symptoms are diagnostic clues rather than definitive proof of a particular failure. More than one factor may contribute to the same surface finish problem.
Dressing conditions influence the cutting edges exposed on a resin bond diamond wheel. Excessive dressing aggressiveness, unsuitable dressing tools, or incorrect relative speeds may damage abrasive grains or produce an uneven working surface.
If effective cutting edges are damaged or unevenly distributed, the wheel may remove material inconsistently. Scratches, local surface defects, and increased grinding forces may follow.
Removing too much material during rework can change the working geometry and affect the relationship between diamond grains and the resin bond. Depending on the bond formulation and dressing method, the resulting surface may have insufficient effective abrasive exposure or an unsuitable cutting structure.
The wheel may then rub or plow the workpiece instead of cutting efficiently. Grinding forces and heat may increase, while material removal and surface finish become less consistent.
Dressing can leave directional or periodic features on the wheel’s working surface. Under certain grinding conditions, these features may be transferred to the workpiece and appear as repeated lines or surface patterns.
This is particularly important in precision grinding, where surface finish and profile accuracy are critical. However, periodic marks can also result from spindle vibration, machine motion, or other process-related factors.
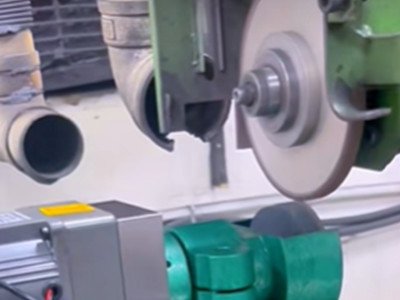
Poor mounting, contaminated flange contact surfaces, excessive runout, or unsuitable balance conditions can cause unstable wheel motion. These issues may generate chatter marks and inconsistent surface roughness, even when the working surface appears acceptable.
Rework that changes the wheel profile or mounting reference may make existing setup problems more noticeable. A wheel should not be assumed to be correctly balanced or safe simply because its profile has been restored.
Resin bond performance depends on the bond formulation, wheel construction, operating temperature, and exposure conditions. Excessive heat during grinding, dressing, or an unsuitable repair procedure may deteriorate the bond or reduce its ability to retain abrasive grains.
Potential warning signs include abnormal abrasive shedding, accelerated wear, visible damage, or a sudden change in grinding behavior. These signs require inspection rather than an assumption that heat is the only cause.
A reconditioned wheel may behave differently from its previous working condition. Changes in profile, abrasive exposure, or effective contact area can influence grinding forces and the response to existing process settings.
Inadequate coolant delivery, poor chip removal, unsuitable feed, or inappropriate wheel speed can also contribute to scratches, loading, heat generation, and unstable surface finish.
A structured inspection helps distinguish wheel-related problems from machine and process issues. The exact procedure depends on the wheel design and the manufacturer’s requirements.
Do not test-run a wheel that is cracked, structurally damaged, or otherwise considered unsafe. Follow the manufacturer’s inspection, mounting, and operating instructions.
Reworking is worth considering only when the wheel remains suitable for the intended application and the expected result can be verified. Replacement may be the better option when the abrasive layer is insufficient, the bond is damaged, the required profile cannot be restored, or the wheel fails safety or dimensional checks.
These are general decision guidelines, not a substitute for the wheel manufacturer’s instructions or a qualified safety assessment.
Possible causes include unsuitable dressing parameters, uneven abrasive exposure, dressing marks, wheel runout, vibration, contamination, and incorrect grinding conditions. Inspect the wheel and machine systematically before deciding which factor is responsible.
Some resin bond diamond wheels can be dressed or reconditioned, depending on their design, remaining abrasive layer, bond condition, and application. The appropriate procedure should be confirmed with the wheel manufacturer.
It can. Material removal, profile correction, mounting errors, or changes in the working surface may affect dimensional accuracy and grinding performance. Relevant dimensions and runout should be checked after rework.
Replacement should be considered when the wheel has structural damage, insufficient abrasive layer, unacceptable bond deterioration, an uncorrectable profile, or performance that cannot meet the required process specifications.
Use the surface roughness measurement method specified for the application. Check the relevant Ra or other required surface parameters, and compare the results with the drawing or process acceptance criteria. Also verify dimensional accuracy and grinding stability where applicable.
Poor surface finish after resin bond diamond wheel rework can result from dressing conditions, abrasive exposure, wheel geometry, mounting and vibration, bond deterioration, or unsuitable grinding parameters. No single cause should be assumed without inspection.
A reliable troubleshooting process combines wheel inspection, machine checks, controlled grinding trials, and surface roughness measurement. Rework should be performed only when the wheel remains suitable for reuse and the procedure follows the manufacturer’s requirements.
Moresuperhard supplies customized diamond grinding wheels for precision grinding applications. For assistance with wheel specifications, dressing requirements, or grinding performance, contact our technical team with your wheel drawing, workpiece material, machine model, and processing requirements.